

ロールフォーミングラインLinia CZS
Zeman




基本データ
価格と所在地
- 所在地:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
オファーの詳細
- 広告ID:
- A21299532
- 更新:
- 最終更新日:22.07.2026
説明
ZEMAN CZS LINE SPECIFICATIONS
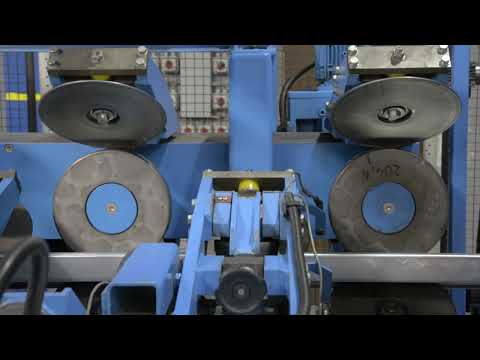
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
Fgsdpeymampjfx Afpeh
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
提供者
最終オンライン:先週
登録日: 2006
188 オンライン広告

お問い合わせを送信
電話 & ファックス


 ドイツ
SpinnerTC 65-MC


 Beograd
GaspariniSlitter


 Eschborn
Deckel MahoDMF 250 linear


 Reiden
GoodwayGS-2800 M


 Blumberg
HWACHEONCutex 160 B


 Weilerswist
TEMAREDCar Flat 3518 für PKW bis 1.438 kg - Kippbar


 ドイツ
GildemeisterCTX 200E

 Fevziçakmak
TFON MACHINE CO.Leveling Machine | TF-L 9016


 Wolfern
ProthPSGC-50120AHR NEUER PREIS!


 ドイツ
SpinnerVC 750

Machineseeker信頼の証
信頼のシールとは何ですか?
Machineseeker は、選ばれた販売店に Machineseeker 信頼シールを認定しています。 発行前に、経験豊富なMachineseekerのスタッフが標準化された包括的な検査を行います。
私たちは何を検査しますか?

営業許可証または商業登記簿抄本の確認
販売者の
郵送先住所の確認
銀行接続の検証
主番号の
電話による
接続可能性の確認
経済情報
には否定的な特徴が含まれていてはなりません
購入者からの苦情
は認証の剥奪につながる可能性がありますこれは購入者としてあなたにとって何を意味しますか?
Machineseekerの信頼シールにより、購入者として自身で確認しなくても、非常に高い確率で誠実かつ公正な取引をしている信頼できるディーラーを見分けることができます。
もちろん、購入プロセス中に意見の相違が生じることもあります。 Machineseekerは、Machineseeker上のアクティブな購入者または販売者による法令違反について責任を負いません。